Featured OEM Custom Container Products
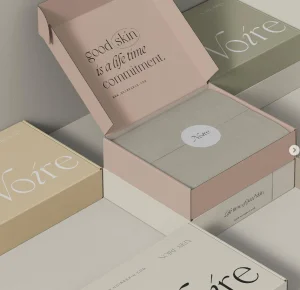
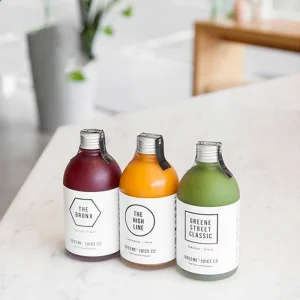
Explore our flagship precision-engineered packaging lines, ranging from high-barrier rigid polymer containers to luxury eco-certified packaging systems.




Global Industrial Landscape: The Evolution of Custom OEM Plastic Container Manufacturing
The global rigid and semi-rigid plastic packaging market has undergone a dramatic structural transformation. Driven by stringent global regulatory standards (such as EU Regulation 10/2011, US FDA Title 21 CFR, and REACH compliance), modern enterprise procurement requires custom OEM plastic container manufacturers to deliver far more than basic spatial containment. Today’s industrial, pharmaceutical, beverage, and cosmetic applications demand sophisticated polymer engineering, precision barrier control, and fully integrated smart packaging compatibility.
Custom OEM (Original Equipment Manufacturer) plastic container manufacturing encompasses a rigorous sequence of polymer science, CAD tool mold engineering, micro-layer co-extrusion blow molding (EBM), injection stretch blow molding (ISBM), and automated high-speed in-mold labeling (IML). Brand owners and industrial supply chain directors must navigate complex tradeoffs between chemical compatibility, impact strength, thermal deflection, moisture vapor transmission rates (MVTR), and oxygen transmission rates (OTR).
Polymers in Modern OEM Packaging: Technical Specification Matrix
Selecting the optimal polymer resin is foundational to OEM container integrity. Below is an engineering comparison matrix designed to guide procurement managers and packaging engineers in selecting materials tailored to specific chemical, thermal, and barrier demands:
| Polymer Type | Density Range (g/cm³) | Barrier Properties (OTR / MVTR) | Thermal Deflection (°C) | Primary Industrial OEM Applications |
|---|---|---|---|---|
| PET (Polyethylene Terephthalate) | 1.34 – 1.39 | High Gas Barrier / Moderate Moisture | 70°C – 75°C | Beverages (PET Cans, Spout Bottles), Pharmaceuticals, Personal Care |
| HDPE (High-Density Polyethylene) | 0.94 – 0.965 | Moderate Gas / Ultra-High Moisture Barrier | 110°C – 120°C | Industrial Chemicals, Detergents, Bulk Rigid Containers, Agro-Chemicals |
| PP (Polypropylene) | 0.895 – 0.92 | Moderate Gas / High Moisture Barrier | 130°C – 140°C (Autoclavable) | Hot-fill Food Containers, Medical Vials, Reusable Hinge Packaging |
| rPET / PCR (Post-Consumer Recycled) | 1.30 – 1.37 | Formulation Dependent (EFSA/FDA Approved) | 68°C – 74°C | Sustainable FMCG Packaging, Eco-conscious E-Commerce & Retail |
Technology Roadmap & Next-Generation Manufacturing Innovation
The technical roadmap of high-performance custom plastic container manufacturing relies on continuous technological advancement across polymer physics, automated molding systems, and smart factory integration.
Micro-Layer Co-Extrusion (EVOH/PA)
Multi-layer container co-extrusion integrates barrier resins like EVOH (Ethylene Vinyl Alcohol) or Polyamide (Nylon) sandwiched between structural polyolefins. This architecture reduces oxygen permeability to less than 0.1 cc/m²/day, drastically extending shelf-life for sensitive pharmaceuticals, carbonated beverages, and liquid nutrients without compromising container recyclability.
High-Precision CAD Tooling & Mold Flow Analysis
Using advanced Finite Element Analysis (FEA) and mold-flow simulations, our structural engineering team optimizes gate placement, cooling channel design, and wall thickness uniformity before physical steel tooling begins. This eliminates stress concentrations, reduces cycle times by up to 25%, and ensures dimensional stability down to ±0.02mm tolerances.
Smart Packaging Integration (RFID / NFC / QR)
Future-proof containers incorporate in-mold embedded RFID tags, tamper-evident smart closures, and high-density 2D barcodes. These enable real-time cold-chain tracking, anti-counterfeiting verification for pharmaceutical peptides and luxury goods, and automated inventory management across international logistics networks.
China Factory Supply Chain Resilience & Shenzhen Vault Box Manufacturing Scale
Shenzhen Vault Box Co., Ltd. was established in 2008 and has developed into a modern, high-tech packaging and printing enterprise specializing in premium customized packaging and plastic container solutions. Operating from the world's most dynamic hardware and manufacturing ecosystem—Shenzhen, China—our company provides global enterprise clients with unparalleled supply chain agility, cost competitiveness, and manufacturing speed.
Equipped with a comprehensive array of automated production systems, Shenzhen Vault Box Co., Ltd. manages an integrated end-to-end manufacturing workflow. Our capabilities span structural design, rapid 3D prototyping, tooling fabrication, precision printing, automated blow/injection molding, rigid post-processing, strict quality inspection, and global delivery logistics.
Workforce & Production Scale
With a dedicated workforce of over 200 highly skilled engineers, polymer technicians, and QC specialists, and a facility spanning approximately 18,000 square meters, Shenzhen Vault Box Co., Ltd. delivers large-scale, high-consistency OEM orders with fast turnarounds. Our mature production management system ensures consistent stability across multi-million unit manufacturing runs.
One-Stop End-to-End OEM/ODM Engineering
Our operational mission focuses on helping global customers elevate product value through innovative, functional, and visually compelling packaging. We deliver full turnkey support including structural engineering consulting, custom tooling design, raw resin blending, mass production, multi-stage QC testing, and door-to-door global logistics support.
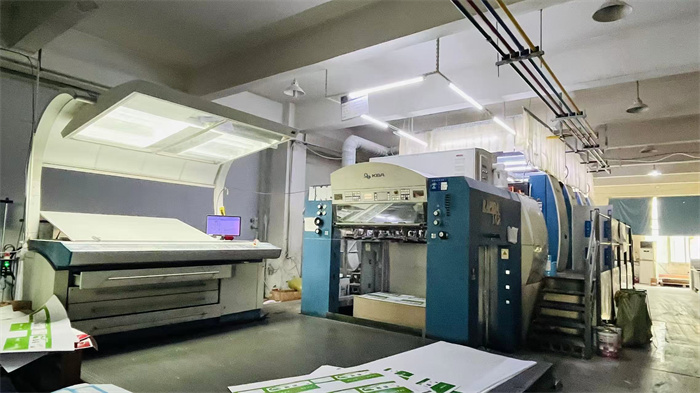
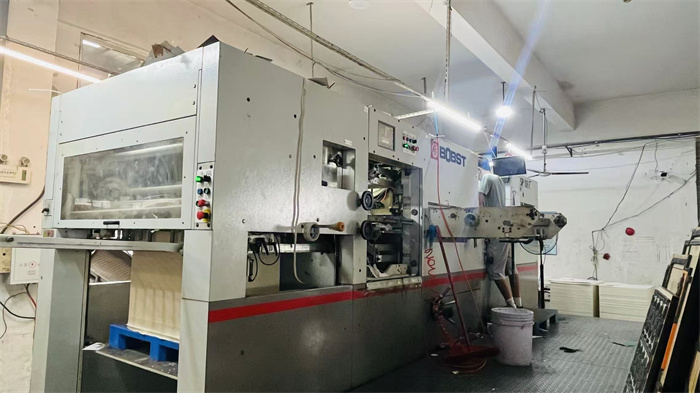
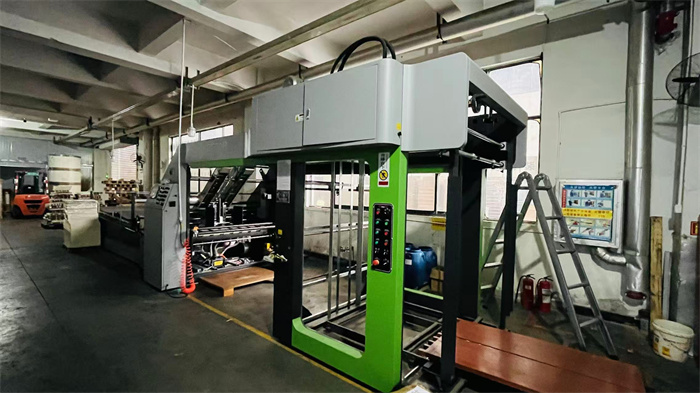
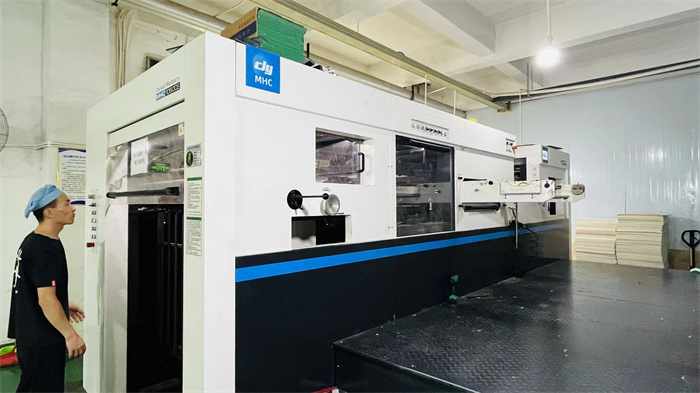
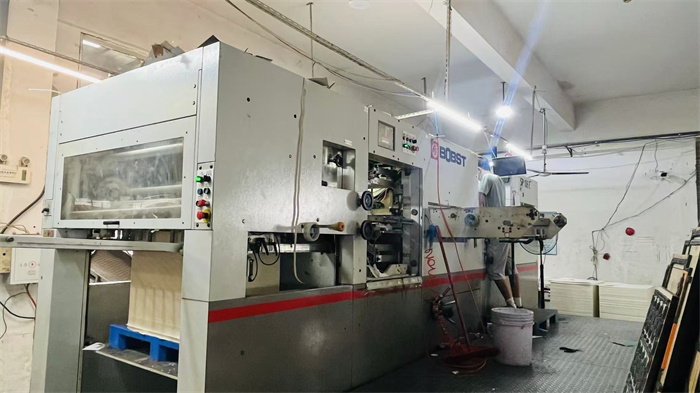
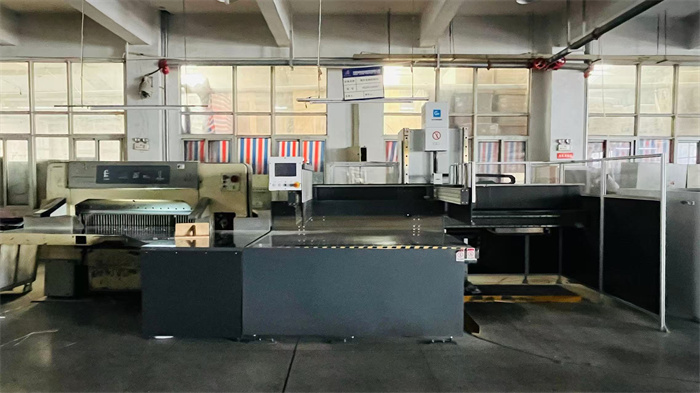
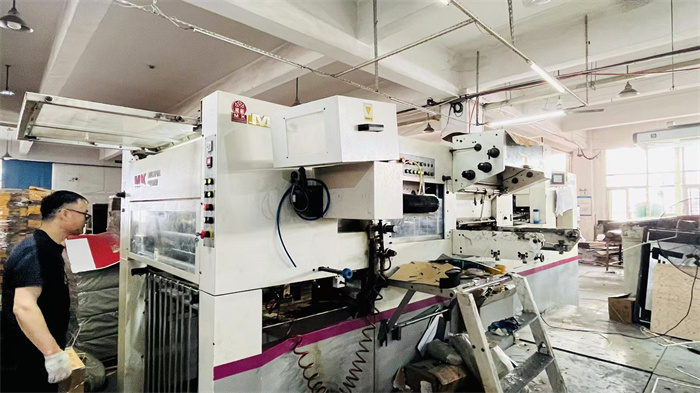
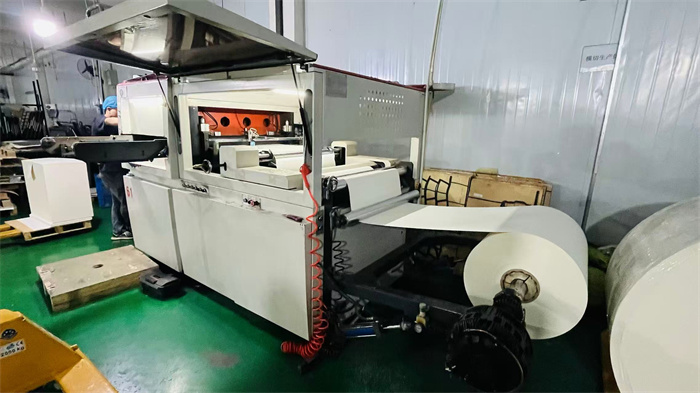
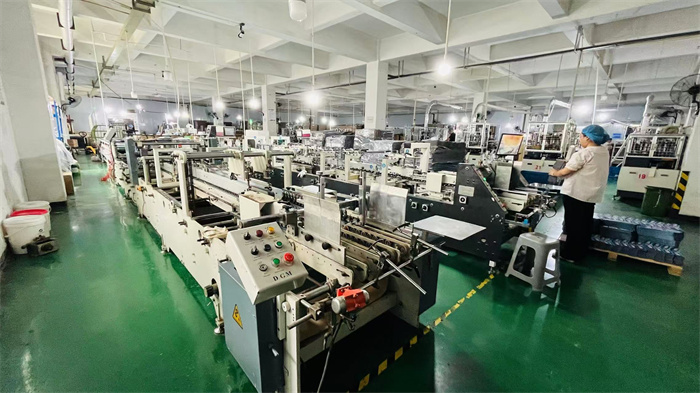
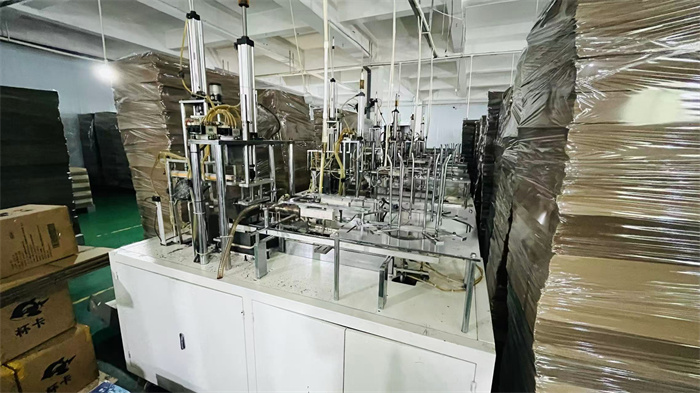
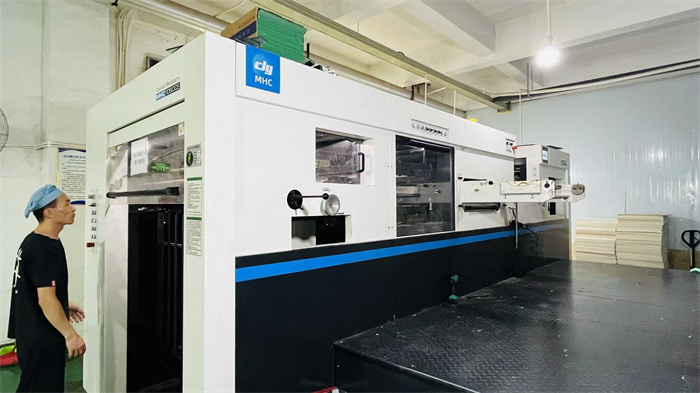
Advanced Manufacturing Infrastructure & Production Equipment
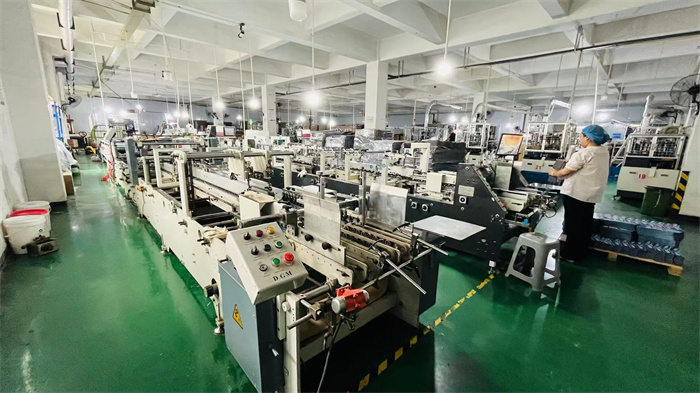
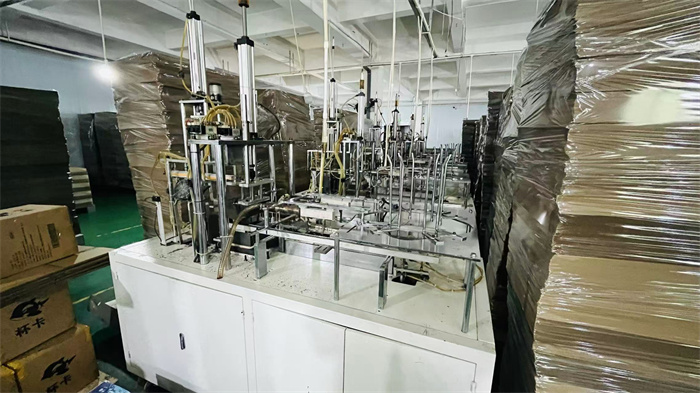
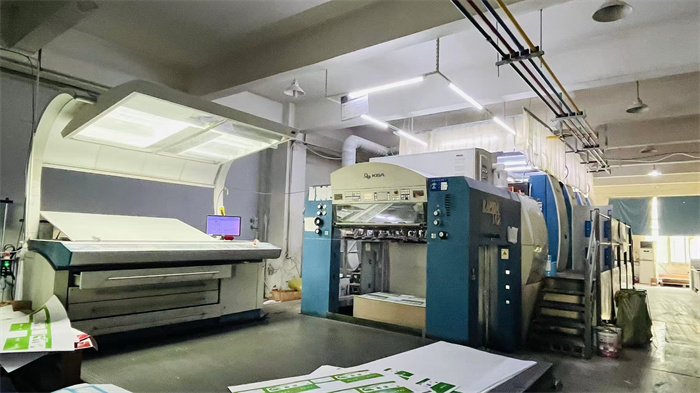
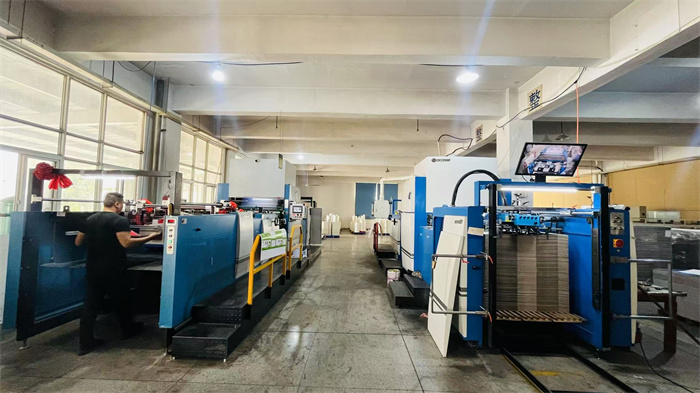
Our 18,000 m² Shenzhen facility houses state-of-the-art machinery lines, including multi-color offset presses, automatic die-cutting machines, precision lamination systems, and high-speed container molding units:
Localized Application Scenarios & Sector-Specific Intent Mining
Custom plastic containers operate across diverse industrial environments, each presenting strict chemical, mechanical, and aesthetic requirements. OEM customization must account for local market preferences, environmental stresses, and regulatory compliance standards.
1. Fast-Moving Consumer Beverages & Food Packaging
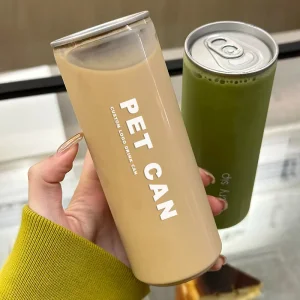
In North American and European retail markets, consumer preference has shifted toward clear, high-transparency PET cans, spout pouches, and recyclable tea/coffee containers. Key engineering criteria include hot-fill structural resistance up to 85°C, high-pressure carbonation containment, and BPA-free food contact certification under FDA 21 CFR 177.1630.
2. Pharmaceutical, Medical & Peptide Packaging
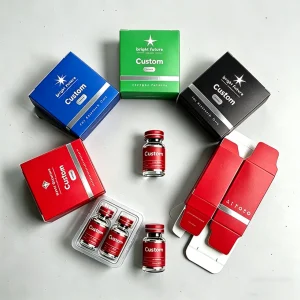
Pharmaceutical packaging demands zero moisture ingress, UV protection, and tamper-evident mechanisms. Our customized peptide boxes, pill bottles, and 3ml/10ml hologram-sealed vial packaging integrate anti-counterfeiting holographic foils, medical-grade USP Class VI polymers, and dust-free cleanroom manufacturing processes to protect sensitive biological compounds.
3. E-Commerce Fulfillment & Rigid Logistics Mailers
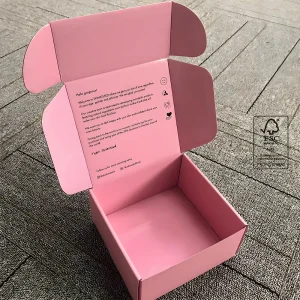
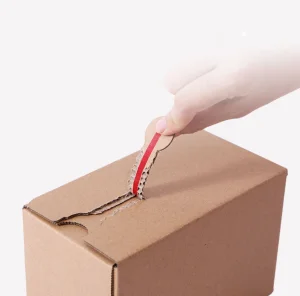
The explosive growth of global cross-border e-commerce (Amazon, Shopify, Western regional fulfillment) demands shipping packaging engineered to survive multi-drop transit. Utilizing corrugated tear-strip mailers, reinforced kraft packaging, and high-impact rigid containers ensures structural stability during parcel transit while reducing volumetric shipping weight.
Global Regulatory Compliance & Sustainability Framework
Exporting custom OEM plastic containers across international boundaries requires strict adherence to global compliance standards and sustainability policies. Shenzhen Vault Box Co., Ltd. continuously invests in eco-friendly raw materials, bio-based polymers, and closed-loop recycling processes.
International Compliance Standards
Our production protocols align with strict international benchmarks:
- US FDA Compliance: Food-contact safe resins meeting 21 CFR standards.
- EU REACH & RoHS: Heavy metal free, non-toxic, chemical safety certified.
- ISO 9001:2015 Quality Management: Documented quality control across every production stage.
- ISO 14001 Environmental Standard: Minimized manufacturing carbon footprint.
Sustainable Material Innovations (PCR & Biodegradables)
To support global carbon neutrality goals, we offer enterprise clients sustainable resin alternatives:
- Post-Consumer Recycled (PCR) PET & HDPE: Up to 100% PCR content options for closed-loop packaging goals.
- Bagasse & Compostable Substrates: Biodegradable food containers derived from natural sugarcane fiber.
- Lightweighting Tool Engineering: Optimized resin wall distribution reducing plastic usage by up to 20% without sacrificing top-load strength.
Frequently Asked Questions (FAQ) & OEM Procurement Guide
Address key technical, logistical, and commercial inquiries regarding custom plastic container manufacturing and OEM collaboration:
More High-Performance OEM Packaging Solutions
Discover our extended portfolio of industrial packaging solutions, including biodegradable food takeaway containers, spout juice pouches, and specialized pharmaceutical peptide packaging boxes.