Featured Heat-Sealed & Custom Packaging Solutions
Explore our engineering-grade custom packaging lineup optimized for structural stability, moisture barrier performance, and brand elevation.


1. Global Industrial State of Custom Heat Sealed Packaging
Analyzing supply chain velocity, barrier thermodynamics, and technical benchmarks driving modern flexible and rigid packaging conversion.
The global heat-sealed packaging market has evolved from elementary protective wrapping into a highly scientific, multi-layered polymer discipline. Driven by shifting consumer dynamics, globalized e-commerce logistics, and stringent pharmaceutical tamper-evident standards, modern OEM heat-sealed packaging manufacturers operate at the convergence of chemical engineering and automated conversion physics. Heat sealing relies on the thermodynamic fusion of thermoplastic interfaces—typically involving Polyethylene (PE), Polypropylene (PP), Polyethylene Terephthalate (PET), or bio-based polymers like PLA—under precise variables of temperature, dwell time, and mechanical pressure.
In modern industrial applications, thermal integrity is evaluated by parameters such as Water Vapor Transmission Rate (MVTR) and Oxygen Transmission Rate (OTR). Advanced thermocompression methods, including constant heat sealing, impulse thermal sealing, and ultrasonic wave fusion, enable factories to engineer bespoke barrier pouches, laminated rigid cartons, and multi-layer structural mailers tailored for specific environmental stresses.
Key Industry Trends Shaping OEM Manufacturing
Mono-Material Circularity
Transitioning from complex non-recyclable multi-material laminates to mono-PE and mono-PP structures with customized low-melting-point sealing layers for 100% recyclability.
High-Speed Automated Conversion
Implementation of continuous rotary heat sealers and servo-driven impulse tools delivering line speeds exceeding 120 units per minute with inline thermal imaging inspection.
Smart Barrier Coatings
Application of nano-thin Al₂O₃, SiOx, and water-based functional dispersion coatings onto paper and film substrates to maintain heat-sealability without compromising recyclability.
2. Industrial OEM Authority: Shenzhen Vault Box Co., Ltd.
Demonstrating E-E-A-T (Experience, Expertise, Authoritativeness, and Trustworthiness) in high-precision packaging fabrication since 2008.
Shenzhen Vault Box Co., Ltd. was established in 2008 and is a modern, high-tech packaging and printing enterprise specializing in premium customized packaging solutions. The company is equipped with a full set of advanced automated production systems, enabling integrated manufacturing capabilities from structural design and creative development to precision printing, post-processing, quality inspection, and final delivery.
With a workforce of over 200 skilled employees and a production facility spanning approximately 18,000 square meters, Shenzhen Vault Box Co., Ltd. has built a strong foundation for large-scale, high-quality, and efficient manufacturing. Over the years, the company has developed mature production management systems and strict quality control standards, ensuring consistency, stability, and excellence in every project delivered. The company supports both domestic and international markets and is capable of undertaking a wide range of legally compliant printed and packaging products.
Our mission is to help customers enhance the value of their products through innovative, functional, and visually compelling packaging. We provide fully customized, one-stop services including packaging consulting, structural engineering, creative design, prototyping, mass production, quality control, and global logistics support. By closely working with clients at every stage, we ensure that each packaging solution aligns with brand positioning and market needs.
Shenzhen Vault Box Co., Ltd. is committed to becoming an industry-leading provider of intelligent and sustainable packaging solutions. We continuously invest in eco-friendly materials, smart packaging technologies, and automated production upgrades to meet evolving global market demands. Innovation and sustainability are at the core of our long-term development strategy. Our business covers multiple key sectors, focusing on delivering tailored packaging solutions that support brand value enhancement and supply chain efficiency.
With a strong focus on quality, innovation, and customer success, Shenzhen Vault Box Co., Ltd. serves global brands and enterprises with reliable, scalable, and value-driven packaging solutions, and continues to build long-term partnerships with clients worldwide.
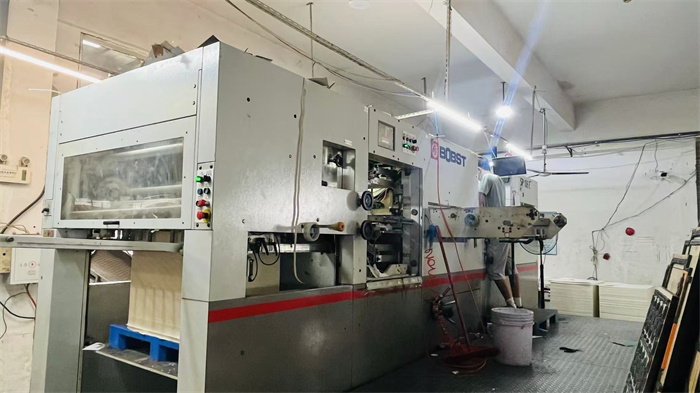
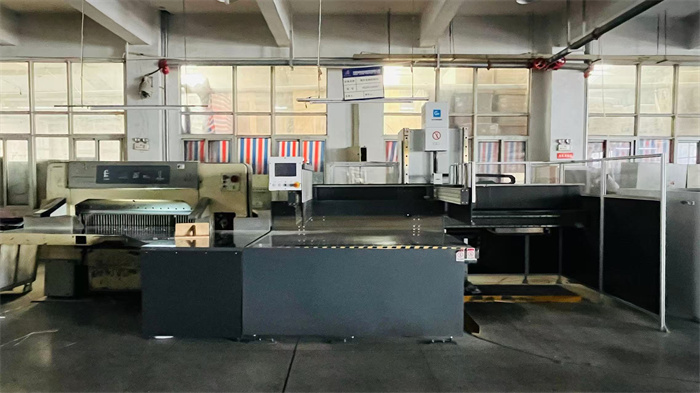
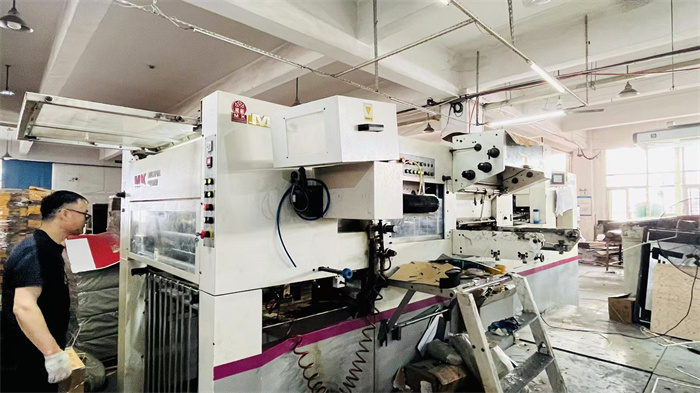
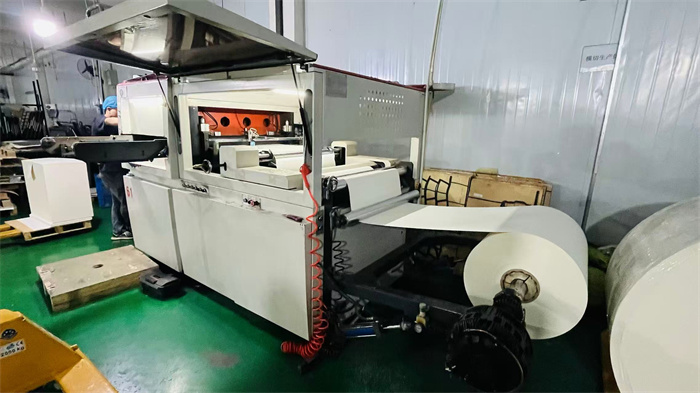
3. Automated Plant Machinery & Manufacturing Process
State-of-the-art six-color printing presses, precision laminating lines, automated die-cutting, and molding infrastructure.
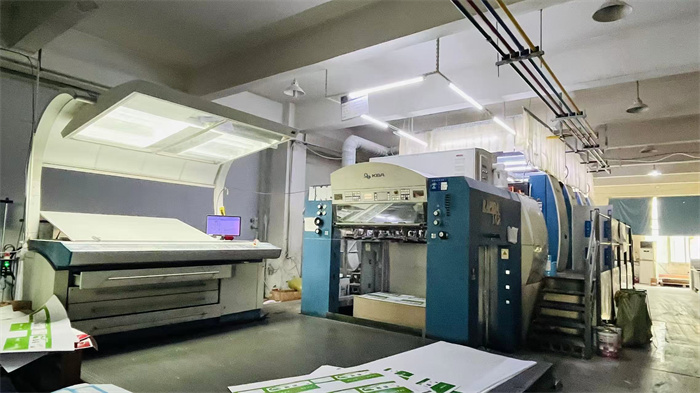
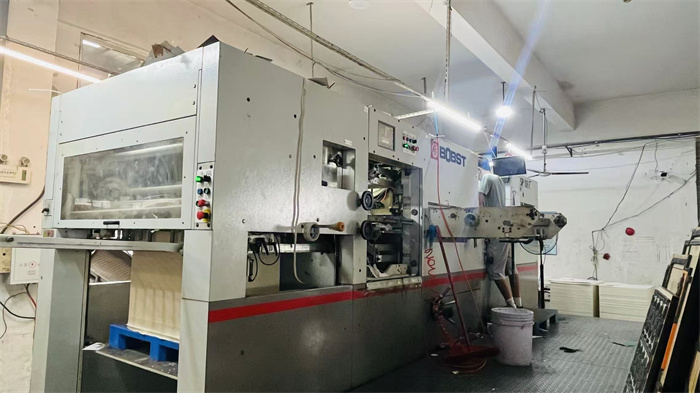
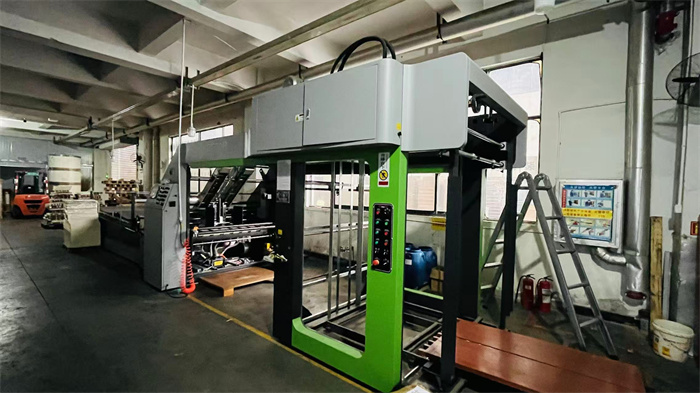
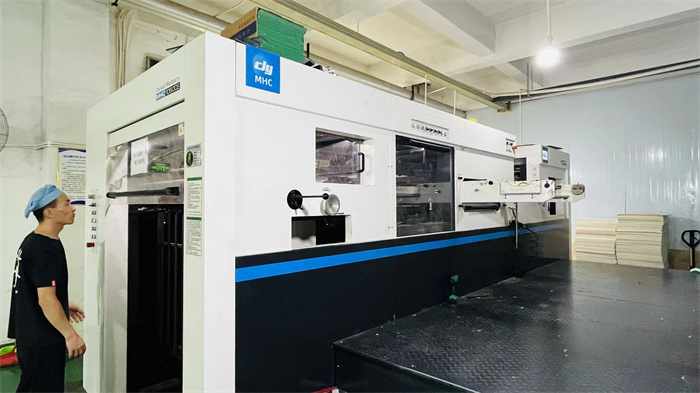
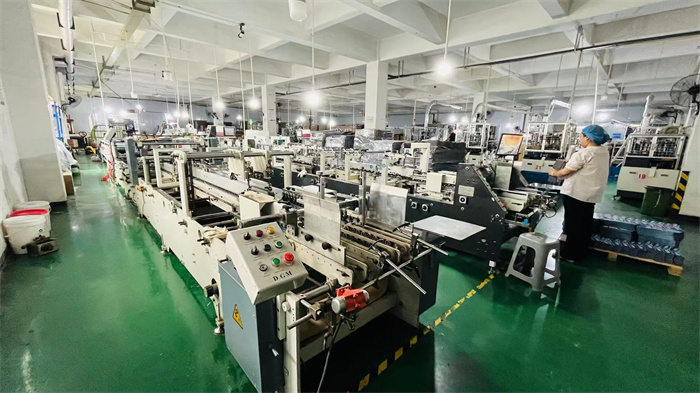
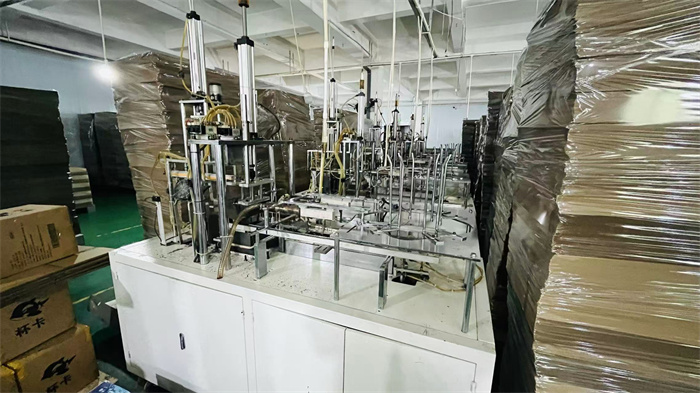
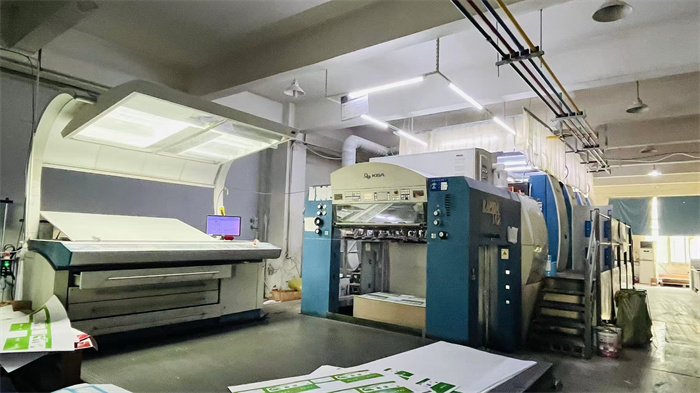
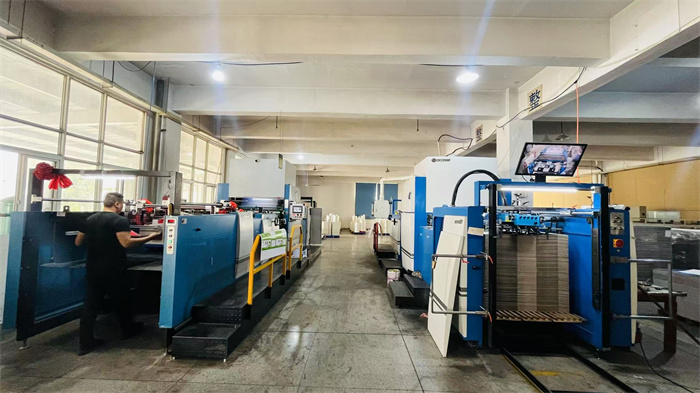
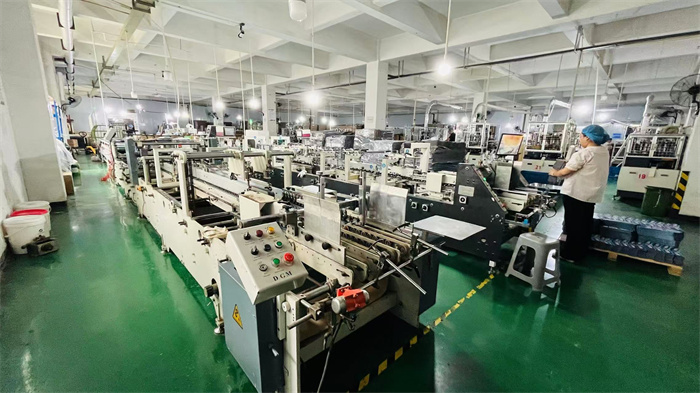
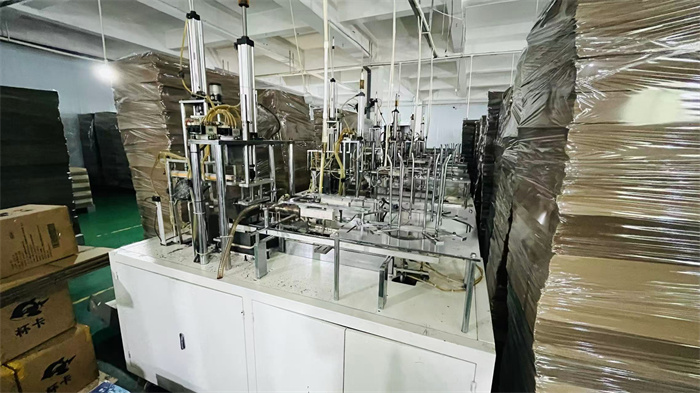
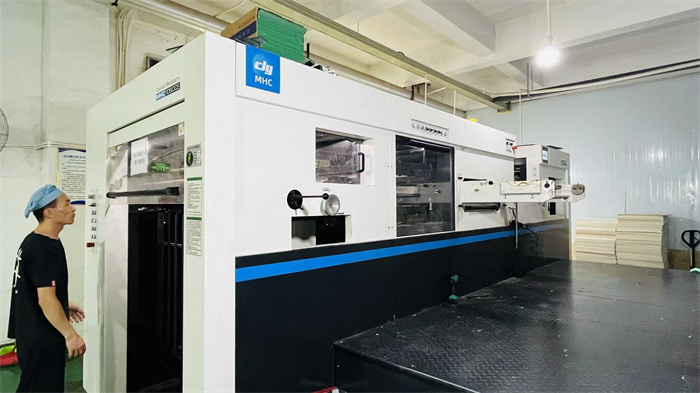
4. Polymer Rheology & Heat Sealing Technical Roadmap
Understanding interface molecular diffusion, seal strength optimization, and heat sealing mechanism dynamics.
Heat sealing is fundamentally a thermo-chemical fusion process wherein polymer chains across two contacting interfaces interdiffuse above their melting temperature (Tm) or glass transition temperature (Tg). The mechanical bond strength achieved is governed by the continuous interaction of heat input, clamping force, and cooling duration. Shenzhen Vault Box Co., Ltd. utilizes rigorous mechanical testing protocols to guarantee peel strength and burst resistance under pressure variation during transport.
| Heat Sealing Technology | Operating Temp Range | Primary Substrate Compatibility | Industrial Advantage | Target Applications |
|---|---|---|---|---|
| Direct Thermal Bar Sealing | 140°C – 220°C | PE, PP, Foil Laminates, Kraft Papers | High continuous output, robust mechanical seal strength | Food Pouches, Bulk Shipping Bags, Heavy Mailers |
| Impulse Heat Sealing | 160°C – 260°C (Burst) | LDPE, HDPE, Thermoplastic Films | Zero warm-up time, energy efficient, minimal heat distortion | Medical Devices, Garment Bags, Poly Mailers |
| Ultrasonic Seal Technology | Friction-based (Cold tool) | Monolayer PE/PP, Bio-resins, Non-wovens | Seals through liquid/powder contamination; zero heat damage | Beverage Pouches, Liquids, High-Speed Flow Wrapping |
| Induction Cap Sealing | 180°C – 250°C (Targeted) | Aluminum Foil Liners + PET/PE Containers | Hermetic non-contact seal, tamper-evident verification | Pharmaceutical Vials, Cosmetics, Chemical Bottles |
Mechanics of Seal Failure Mitigation
Quality control in heat sealing focuses on overcoming three primary defect vectors: micro-channel leaks, thermal burn-through, and delamination. Through our advanced automated lamination and six-color printing systems, Vault Box controls adhesive weight distribution down to ±0.1 g/m², preventing micro-voids during post-seal thermal contraction.
5. Comprehensive Macro Sector Application Framework
Custom OEM configurations tailored to specific international regulatory and industrial demands.
E-Commerce & High-Speed Fulfillment
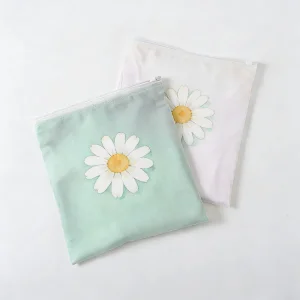
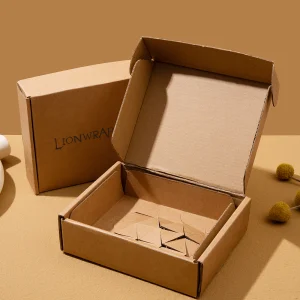
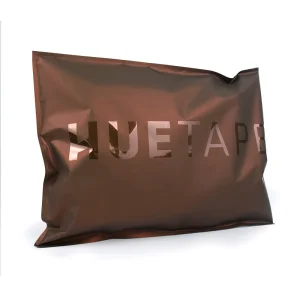
Custom printed poly mailers and corrugated mailer boxes featuring self-seal heat-melt adhesive bands, tear-strip opening, and metallic moisture barriers for global shipping protection.
Luxury Cosmetics & Fragrance Packaging
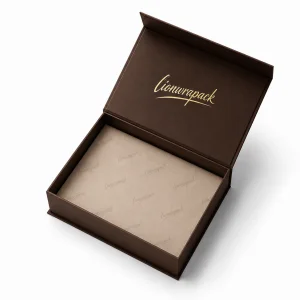
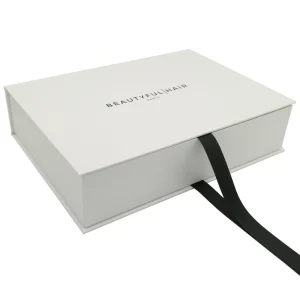
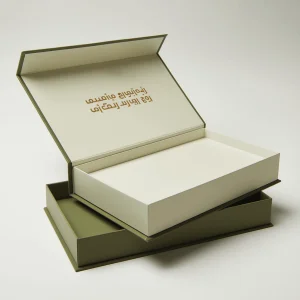
Rigid cardboard folding cartons, magnetic closing gift boxes, and perfume bottle packaging featuring gold foil pressing, custom foam/plastic inserts, and pristine surface finishes.
Medical & Pharmaceutical Integrity
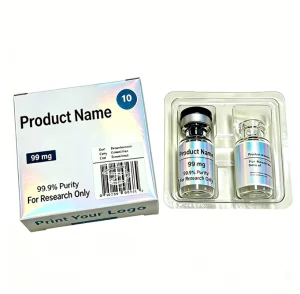
Sterile-grade peelable heat sealed pouches, paper-board vial boxes, and waterproof pill pack containers meeting international compliance for seal hermeticity and child resistance.
Food & Beverage Pulp Preservation
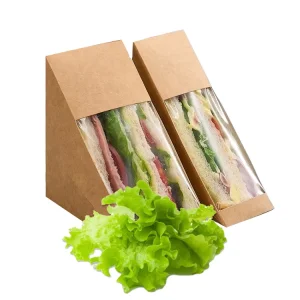
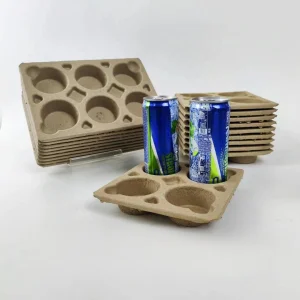
100% Biodegradable paper pulp containers, spout stand-up pouches for liquids, and food-grade kraft sandwich boxes engineered with heat-sealable oil and moisture protection barriers.
Industrial Packaging & Protective Cushions
Heavy-duty honeycomb kraft paper mailer boxes, ESD-shielded heat sealing barrier bags, and molded pulp shock absorbers designed for extreme transport stress.
6. Technical Roadmap & Sustainability Commitment
Pioneering bio-polymer thermal fusion, zero-waste die-cutting, and smart AI vision inspection.
As regulatory frameworks like the European Union Packaging and Packaging Waste Regulation (PPWR) enforce stringent plastic reduction targets, Shenzhen Vault Box Co., Ltd. is advancing next-generation sustainable thermal barriers. Our R&D division focuses on three main pillars:
Bio-Based Polyesters & PLA
Developing low-temperature thermal seal coatings derived from polylactic acid (PLA) and polyhydroxyalkanoates (PHA) that compost naturally within 180 days while maintaining grease proofing.
AI Inspection Systems
Integrating online infrared thermal sensors to evaluate 100% of seal seams during high-speed production, instantly detecting temperature fluctuations and micro-voids.
Material Reduction Science
Engineering lightweight corrugated flutes and ultra-thin flexible barrier films without compromising structural crush resistance or hermetic burst ratings.
Frequently Asked Questions (FAQ)
Technical guidance for B2B procurement managers, packaging engineers, and enterprise buyers.
Additional OEM Packaging Solutions Portfolio
Explore our complete catalog of leak-proof pouches, rigid boxes, and protective mailers.